The best beverage manufacturer for private label drinks in China is the contract producer that matches your formulation, packaging format, and volume targets while holding verifiable food-safety certifications. For most brands sourcing at scale, a China-based co-packer offers the strongest combination of low per-unit cost, broad format range, and export-ready logistics. The right choice depends on your category, your order size, and how much formulation support you need from the factory.
Selecting a beverage manufacturer for private label drinks business growth means looking past price alone. You are choosing a long-term production partner whose quality controls, lead times, and compliance records become part of your brand. This guide breaks down what separates a reliable co-packer from a risky one, why China remains a leading sourcing region, and how to evaluate cold-fill, hot-fill, and bulk capabilities before you commit.
| Building a private label drink line and need durable, condensation-proof label stock for your bottles and cans?Talk to Vizlent’s beverage labeling engineers today |
What a Private Label Beverage Manufacturer Actually Does
The best beverage manufacturer for private label drinks in china produces finished drinks that you sell under your own brand name rather than theirs. These contract producers handle sourcing, blending, filling, sealing, and often packaging, so your team can focus on branding and distribution. The arrangement lets new and established brands enter the market without building a costly bottling plant from scratch.
Most contract producers fall into two groups: co-packers who fill your supplied recipe, and full-service houses who develop the formula with you. A full-service beverage manufacturer for private label drinks companies often can support R&D, nutritional paneling, and regulatory review in one place. Knowing which model you need keeps your sourcing search focused and your quotes comparable.
Core services to expect
- Formulation and R&D: recipe development, flavor matching, and shelf-life testing for new SKUs.
- Filling and packaging: cold-fill, hot-fill, and aseptic lines across cans, glass, and PET formats.
- Compliance support: nutritional analysis, label review, and documentation for target export markets.
- Logistics: palletizing, export packaging, and freight coordination to your warehouse.
Why China Leads in Private Label Beverage Production
A beverage manufacturer for private label drinks China brands rely on usually offers lower unit costs than producers in North America or Europe. Decades of investment in food-grade processing, canning, and PET lines have built deep manufacturing capacity across coastal provinces. This scale lets Chinese co-packers price competitively even on mid-size runs while still meeting international standards.
China is also a sourcing advantage for ingredients, packaging, and finished-goods logistics in one corridor. Many factories sit close to the can, bottle, and closure suppliers they depend on, which shortens lead times and reduces freight inside the supply chain. For a beverage manufacturer for private label drinks bulk orders, that proximity often translates into faster turnaround and consolidated shipping.
Where China stands out as Best Beverage Manufacturer for Private Label Drinks
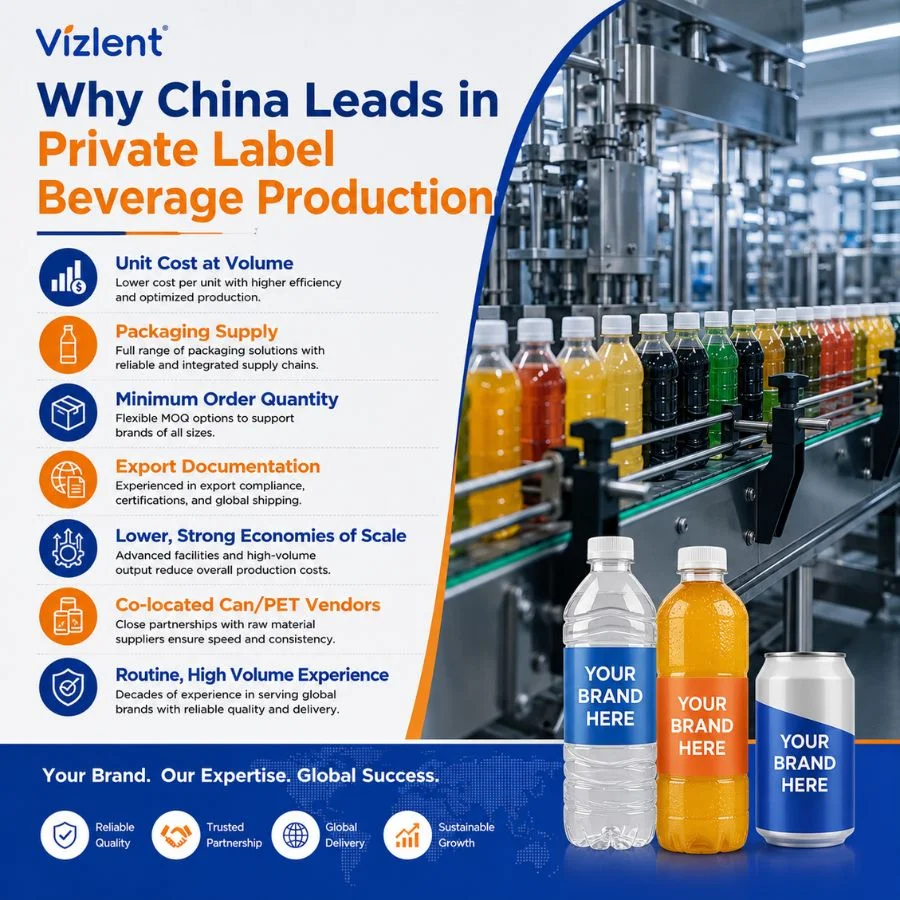
| Sourcing factor | China-based co-packer | Typical Western co-packer |
|---|---|---|
| Unit cost at volume | Lower, strong economies of scale | Higher labor and overhead |
| Packaging supply | Co-located can/PET vendors | Often sourced separately |
| Minimum order quantity | Flexible across many factories | Frequently higher entry MOQs |
| Export documentation | Routine, high-volume experience | Varies by producer |
These advantages do not remove the need for diligence. A low quote means little if the factory cannot show current certifications or a clean audit history. Treat China as a strong starting region, then qualify each candidate on the criteria below.
Cold-Fill, Hot-Fill, and the Formats That Define Your Choice
A beverage manufacturer for private label drinks cold processing lines fills products that stay shelf-stable without heat, such as flavored waters, juices with preservatives, and many functional drinks. Cold-fill protects heat-sensitive vitamins, botanicals, and flavors that pasteurization can degrade. If your product carries delicate actives or fresh flavor notes, cold-fill capability moves to the top of your checklist.
Hot-fill and aseptic lines, by contrast, use heat to kill microbes so juices, teas, and dairy-style drinks stay safe at ambient temperature. Each method demands different equipment, container types, and validation records from the factory. Confirm that a candidate runs the exact fill method your formula requires before you compare any prices.
Match the format to the process
- Cold-fill: flavored water, sports drinks, and many functional beverages with vitamins or botanicals.
- Hot-fill: juices, iced teas, and sauces that need heat for shelf stability.
- Aseptic: dairy alternatives and sensitive nutrient drinks filled in sterile conditions.
- Carbonated: sodas, sparkling waters, and energy drinks needing pressure-rated cans or bottles.
| Cold-fill, hot-fill, or ice-bucket distribution? Your label has to survive the same conditions your drink does.Request beverage label samples built for condensation and immersion |
How to Vet The Best Beverage Manufacturer for Private Label Drinks in China Before You Commit

Vetting starts with certifications, because food safety is non-negotiable for any beverage manufacturer for private label drinks and beverages. Ask for current documentation and confirm the certificates cover the exact site producing your order. A factory that hesitates to share audit records is telling you something important early.
Next, test capability with a sample run rather than a spec sheet alone. A short trial reveals fill accuracy, seal integrity, and how the team handles your formula under real line conditions. Pair that trial with reference checks from brands already shipping products through the same factory.
The diligence checklist
- Certifications: GMP, HACCP, and ISO 22000 or FSSC 22000 appropriate to your market.
- Audit history: recent third-party reports and any corrective actions taken.
- Sample run: a paid trial batch to validate fill, seal, and finish before scaling.
- References: two or more current clients in a similar category and volume band.
- Capacity headroom: room to grow with you without missing existing commitments.
Certifications that signal a serious producer
| Certification | What it verifies | Why it matters |
|---|---|---|
| HACCP | Hazard analysis and control points | Systematic safety across the process |
| ISO 22000 / FSSC 22000 | Food safety management system | Recognized by global retailers |
| GMP | Good manufacturing practices | Consistent hygiene and process control |
| BRCGS | Brand and consumer protection standard | Often required by large retail buyers |
Bulk Orders, MOQs, and Pricing You Can Plan Around

Minimum order quantities shape which partners you can realistically use as a beverage manufacturer for private label drinks bulk suppliers. Minimum Order Quantity (MOQs) vary widely, from a few thousand units at a flexible co-packer to full truckloads at a high-volume plant. Match the MOQ to your forecast so you are not sitting on inventory or constantly reordering.
Per-unit pricing usually drops as volume rises, but the full landed cost includes ingredients, packaging, freight, and duties. Build a complete cost model before you compare quotes, because a low factory-gate price can lose its edge after shipping. A transparent producer will walk you through each cost line rather than hiding it inside a single number.
Cost lines to model before signing
- Unit production: Filling, blending, and finishing per case at your target volume.
- Packaging and labeling: Cans or bottles, closures, and durable label stock.
- Freight and duties: Ocean or air freight, customs, and inland delivery to your hub.
- Tooling and setup: Any one-time line changeover or custom mold charges.
Don’t Overlook the Label: The Part Buyers Touch First
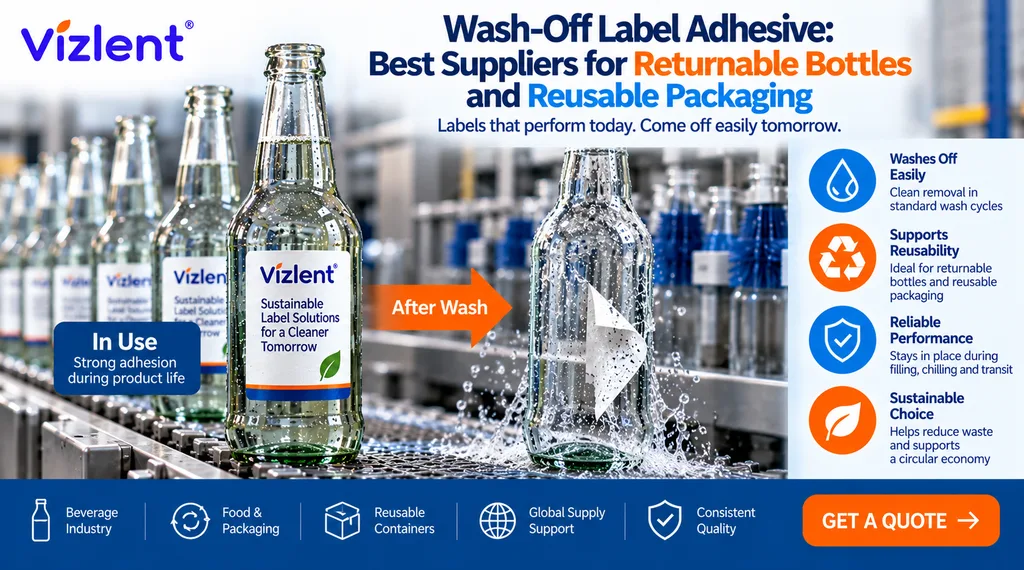
The drink inside the bottle wins repeat sales, but the label is what a shopper sees and grabs in a cold case. Beverage labels face condensation, ice-water immersion, and high-speed application that ordinary paper stock cannot survive. A label that curls or slides off in a cooler quietly undermines the quality message your product worked to earn.
This is where your label material supplier becomes as important as your beverage manufacturer. Wet-strength paper and laminating films keep print sharp and adhesion firm through filling, chilling, and handling. Specifying the right face stock and adhesive up front prevents costly relabeling and shelf rejections later.
Label properties that matter for drinks
- Low-temperature adhesives that bond to cold, damp glass and PET on the line.
- Wet-strength and biodegradable face stocks for sustainability claims without losing durability.
- Condensation and immersion resistance for beer and beverage labeling in ice buckets and coolers.
- High-speed runnability so labels track cleanly through rotary applicators at full line speed.
Private Label Across the Beverage Alcohol Industry
The beverage alcohol industry runs on private label production as much as the non-alcoholic side does. Retailers, restaurants, and emerging brands commission contract producers to make beer, hard seltzer, ready-to-drink cocktails, and wine under their own labels. The same vetting logic applies, with added attention to excise compliance and category-specific licensing.
Labeling demands climb higher here, since alcohol products face strict regulatory content rules and harsh distribution conditions. Bottles and cans move through ice, condensation, and rough handling that test both adhesive and print. A producer and a label supplier who both understand the beverage alcohol industry reduce your compliance and quality risk at once.
Extra considerations for alcoholic private label
- Regulatory labeling: Mandatory statements, ABV, and warnings that vary by market.
- Excise and licensing: Duty handling and permits specific to your destination countries.
- Durability: Labels that hold through ice immersion, condensation, and transit abrasion.
| Sourcing alcohol or RTD private label products? Your cans and bottles need labels rated for ice, condensation, and high-speed fills. Get a quote on beverage-grade label stock from Vizlent |
Get Beverage Label Stock Built for the Cold Case
Choosing the right beverage manufacturer for private label drinks business success is half the equation; the label that survives filling, chilling, and handling is the other half. Vizlent manufactures wet-strength, low-temperature, and laminating label materials engineered for condensation, ice immersion, and high-speed beverage lines. As a China-based, ISO 9001, FSC, and SGS-certified label stock producer since 2011, Vizlent Label Materials Co., Ltd. supplies converters and brands across 50+ countries.
| Ready to put a label on your private label drink that holds up from filling line to consumer hand? Send your inquiry to Vizlent’s beverage labeling team now |
Frequently Asked Questions
What is the best beverage manufacturer for private label drinks?
The best beverage manufacturer for private label drinks is the certified co-packer whose fill method, formats, and MOQ match your product and volume. There is no single winner for every brand. China-based producers often lead on cost and format range, but the right fit always depends on your category, order size, and the formulation support you need.
Why do so many brands source private label drinks from China?
A beverage manufacturer for private label drinks china brands usually combines lower unit costs, broad format capability, and export-ready logistics. Decades of investment in food-grade canning and PET lines built deep capacity. Co-located packaging suppliers also shorten lead times, which helps both small trials and large bulk runs.
What is the difference between cold-fill and hot-fill production?
A beverage manufacturer for private label drinks cold-fill line fills products that stay stable without heat, protecting vitamins and delicate flavors. Hot-fill uses heat to kill microbes for ambient shelf stability. Your formula decides which you need, so confirm the exact method before comparing prices between producers.
How do I check if a beverage manufacturer is reliable?
Ask for current certifications such as HACCP, GMP, and ISO 22000, and confirm they cover the exact production site. Request a paid sample run to test fill accuracy and seal integrity. Then check references from current clients in your category and volume band before committing to a full order.
What are typical minimum order quantities for private label beverages?
MOQs for a beverage manufacturer for private label drinks bulk order range from a few thousand units at flexible co-packers to full truckloads at high-volume plants. Match the MOQ to your sales forecast. Smaller trial runs cost more per unit but reduce the risk of holding excess inventory early on.
Do private label beverage manufacturers help with formulation?
Many do. A full-service beverage manufacturer for private label drinks companies can develop recipes, run shelf-life testing, and build nutritional panels in house. Co-packers, by contrast, fill a recipe you supply. Decide which model you need so your quotes stay comparable across candidates.
What should I look for in beverage labels for private label drinks?
Choose label stock rated for condensation, ice-water immersion, and high-speed application. Low-temperature adhesives bond to cold, damp containers, and wet-strength face stocks keep print sharp. Specifying durable material up front prevents labels from curling or sliding off in coolers and avoids costly relabeling.
Does private label production work for the beverage alcohol industry?
Yes. The beverage alcohol industry widely uses contract producers for beer, hard seltzer, ready-to-drink cocktails, and wine. The same vetting steps apply, with added focus on excise compliance, licensing, and regulatory labeling. Durable, immersion-resistant labels are especially important for alcohol products in chilled distribution.