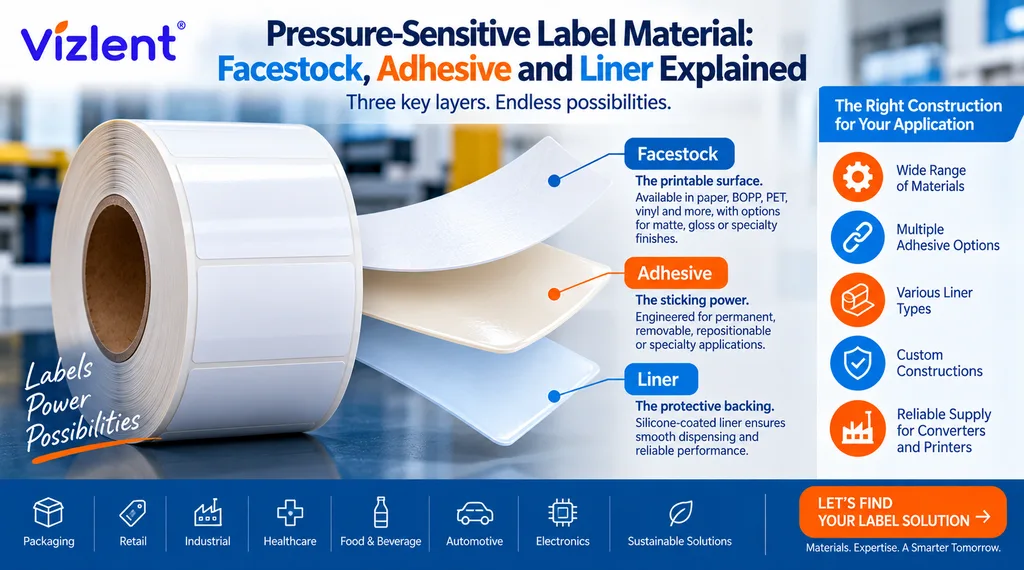
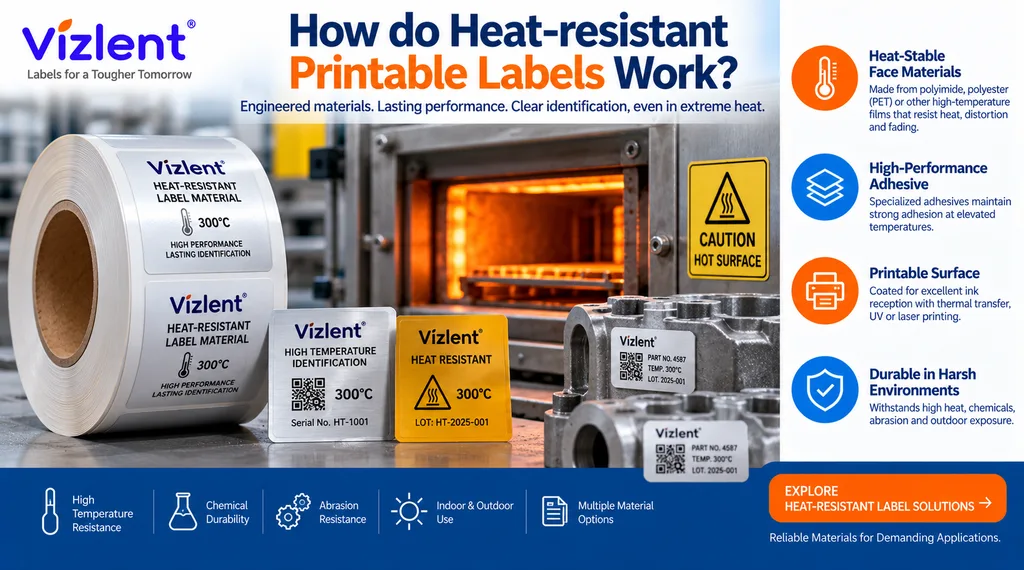
Heat-resistant printable labels work by pairing a facestock that holds its dimensions and surface at temperature with an adhesive that keeps bonding at that same temperature, then adding a print system whose image does not soften, smear or fade under the same heat. Take any one of those three away and the label fails. In most constructions the adhesive is the first component to reach its limit, which is why a label rated for a hot process is specified as a complete construction rather than as a single material.
The confusion in the market comes from treating “heat resistant” as a property of the facestock alone. A polyester film can tolerate an oven that its adhesive cannot. A polyimide label can survive a reflow profile while its printed image flakes because the wrong ribbon was fitted, so heat resistant labeling is a systems decision rather than a material choice.
The Three Layers That Decide Heat Performance
| Layer | What it controls | Key variables to specify |
|---|---|---|
| Facestock | Dimensional stability, shrinkage, embrittlement, surface integrity | Polymer type, caliper, top-coat, peak and continuous temperature |
| Adhesive | Whether the label stays on, or releases on purpose | Chemistry, coat weight, substrate surface energy, application temperature |
| Print system | Whether the image survives the process | Printer type, ribbon or toner chemistry, print energy, abrasion and chemical exposure |
Indicative only. Confirm every value against the technical data sheet for the specific construction you are quoting.
Ready to skip the guesswork? Send your process temperature and substrate to Vizlent and get a recommended construction back with its data sheet.
What Makes a Facestock Heat Resistant
A facestock earns a heat rating from its polymer backbone, not from a coating sprayed on afterwards. Polyimide films hold their mechanical properties far above the point where common label films distort, which is why they appear on circuit boards. Polyester holds a useful middle ground, and biaxially oriented polypropylene and PVC sit well below both.
Vizlent currently publishes construction ratings on its heat resistant label category page that make the spread visible. At the time of writing that page gives an engineered polyimide construction as continuous to 300°C (572°F) with short spikes to 350°C, a vulcanized film construction to 210°C (410°F), and a polyester construction to 150°C (302°F). Those figures belong to the named constructions rather than to the polymer families in general, so a polyester label is not rated to 150°C simply because it is polyester.
- Polyimide: highest published rating in the polymer range, selected for PCB and electronics assembly
- Polyester (PET): the workhorse for heat resistant printer labels in ovens, motors and under-hood positions. Vizlent currently publishes premium PET film at 1.0 to 5.0 mil with a service range of -40°F to 300°F on its self-adhesive material page
- Vulcanized film: built to bond into rubber during curing, covered under vulcanized rubber labels
- Metal foil and aluminium constructions: selected where the requirement exceeds what common polymer label materials can carry. The important qualification is below
- Flame-retardant grades: a separate requirement from heat resistance, on the flame retardant label range
Why a Metal Facestock Does Not Set the Label’s Rating
Metal foil and anodized aluminium tolerate temperatures far beyond any polymer film, and Vizlent’s heat resistant category page cites aluminium foil and metalized tag applications above 600°C (1112°F) in metallurgy and steel processing. That figure describes what the metal substrate can be selected for, and it is published without stated test conditions on that page. A complete pressure-sensitive label does not inherit it.
The full construction is metal plus adhesive plus coating plus imaging system, and the adhesive or the printed mark usually becomes the limiting component long before the metal does. Treat any figure above the polymer range as an application indication rather than a construction rating. Ask for the specific construction, its tested exposure and the stated test conditions before you design around it.
Top-coats matter as much as the polymer, because the top-coat is the surface the ink anchors to. A film can carry a strong temperature rating and still shed its printed image on first handling if the coating is not receptive to the print method. Ask specifically whether the top-coat is qualified for the printing route you intend to use.
Why the Adhesive Usually Reaches Its Limit First
In many pressure-sensitive constructions, the adhesive becomes the limiting component before the facestock reaches its thermal limit. Softening shows up as edge lift long before anyone notices the film itself changing. Heat drives two things at once: the adhesive loses cohesive strength, and the substrate underneath expands at a different rate than the label, and the resulting shear at the label edge is what peels corners in a curing oven.
High-temperature acrylics handle the middle of the range and hold up well against solvents and cleaning chemistry. Silicone pressure-sensitive adhesives can provide higher-temperature performance and flexibility in constructions designed for severe thermal exposure, which is why they appear alongside polyimide. For textured metals and low surface energy plastics, a heavier adhesive coat weight is often selected so the adhesive can wet a surface that resists it, and Vizlent’s durable label range covers those constructions.
Application Temperature Is a Separate Specification
Minimum application temperature and maximum service temperature are two different numbers, and buyers routinely conflate them. An adhesive rated to a high service temperature may still require application above a specified minimum temperature to wet the surface and build a bond. Applying a heat resistant label sticker to a cold part and then heating it is a common route to failure that looks like an adhesive defect.
Dwell time before the first heat exposure is the other variable that gets skipped. Many permanent acrylics develop higher adhesion after application and a period of dwell. Labels applied and sent straight into an oven may never reach their published bond, so ask what dwell the published figure assumes and build that into your line sequence.
Not sure whether your failure is adhesive, application or process? Request a Vizlent sample roll and run it against your real profile before you commit to volume.
How to Print Thermal Labels That Survive the Heat
Learning how to print thermal labels for high-temperature service starts with imaging chemistry. For sustained high-temperature applications, direct thermal is generally unsuitable because its imaging layer is heat-sensitive by design. The same coating keeps reacting whenever heat reaches it, so a direct thermal label near an oven, a motor or a heat gun darkens across its whole face and becomes unreadable.
Thermal transfer with a full resin ribbon is the method used for heat resistant labeling, because resin ink fuses to the facestock rather than reacting inside it. Vizlent currently publishes three formulations on its high temperature ribbon page: a standard high-heat resin to 200°C (392°F) on PET and PVC, a polyimide tracking resin to 300°C (572°F), and an ESD-safe anti-static resin to 260°C (500°F), on a 4.5 to 5.7 µm PET base film. The same page gives an ink melting point above 110°C, which is why these ribbons ask for high printhead energy and a reduced print speed.
- Match the ribbon to the facestock, not just to the printer. A resin formulated for polyimide will not necessarily anchor to a coated polyester
- Raise printhead energy and slow print speed for dense barcodes, then verify print quality against an applicable method such as ISO/IEC 15416:2025 (Edition 3, January 2025) for linear symbols
- Confirm printable area and ribbon width against the printer manufacturer’s specification rather than assuming ribbon width follows material width
- Test legibility after the actual heat cycle, not before it
- Compare options across the thermal transfer ribbon and resin ribbon ranges when specifying
Laser, Inkjet and Marking Alternatives
Laser printing suits low-volume and on-demand work. Vizlent’s heat-resistant printable labels product page describes a high-temperature polyester construction with a permanent adhesive, aimed at laser printing and resistant to oils and chemicals. Toner fuses under heat and pressure inside the printer, which gives a durable image without a ribbon inventory, at the cost of throughput and a facestock that must be qualified not to curl or shrink in the fuser.
Where no printed image will survive, marking replaces printing, and laser etched constructions put the mark into the material instead of onto it. Inkjet sits between the two and needs a receptive coating plus an ink chemistry qualified for the exposure, so it is specified case by case. For heat-resistant printable stickers used in less severe positions, a resin-printed polyester usually remains the more economical answer.
Are Vinyl Stickers Heat Resistant? A Direct Answer
Are vinyl stickers heat resistant? In general terms, no, not at industrial process temperatures. Vizlent currently publishes flexible PVC vinyl at a service range of -20°F to 180°F, roughly 82°C at the top end, on its self-adhesive material page, which covers warm environments and hand contact but not ovens, soldering or curing.
Vinyl earns its place for conformability and outdoor durability rather than heat, which is why it dominates decals and equipment marking on the outdoor weather resistant range. Above that published range, plasticiser migration, shrinkage and adhesive softening begin to show. If a decal has to enter a paint bake, a wash tunnel or an engine bay, polyester or polyimide is the correct family and vinyl is not.
- Reasonable for vinyl: ambient outdoor, warm storage, appliance exteriors, general equipment marking
- Not suitable for vinyl: powder coat, paint bake, reflow, autoclave, steam lines, exhaust proximity
Matching Ratings to Real Processes
A temperature rating means little until it is matched to a documented process profile. Electronics assembly provides a useful example, because IPC/JEDEC J-STD-020F, published in December 2022, defines moisture and reflow sensitivity classification profiles for non-hermetic surface-mount devices. Its classification peak package body temperatures of 245°C, 250°C or 260°C vary with package thickness and volume, with time above the 217°C liquidus commonly specified at 60 to 150 seconds.
That standard classifies packages rather than setting a universal label requirement, so treat it as a description of the thermal environment your label will see rather than as a label specification. A label riding a board through such a profile still has to hold its adhesive, its dimensions and its barcode grade at those temperatures. Confirm the actual profile your assembler runs, since it may differ from the classification profile.
Sterilization, Ovens and Powder Coat
Sterilization is a different shape of exposure: lower temperature, but with steam, pressure and repeated cycles. ISO 17665:2024 sets requirements for the development, validation and routine control of moist heat sterilization processes rather than mandating a temperature. In practice, common moist-heat cycles can operate around 121°C to 134°C depending on the validated process and the device requirements, and repeated wet cycles attack adhesives differently from a single dry spike.
Paint bake and powder coat cycles combine sustained heat with substrate expansion, and the label is usually applied to bare or primed metal before the part enters. This is where a label on a low surface energy or textured surface needs a heavier coat weight to stay wetted through that expansion. Edge lift, rather than total loss, is the realistic risk.
What UL 969 Recognition Actually Covers
UL 969, Marking and Labeling Systems, is currently Edition 6, published 24 July 2025, with a revision dated 28 July 2025. It evaluates legibility, resistance to defacement and minimum adhesion performance for specific combinations of material, ink and printing or imaging process. Any recognition applies to that evaluated combination and its stated conditions of acceptability, which name the application surfaces, use conditions, minimum and maximum exposure temperatures and any chemical exposures.
The practical consequence is that recognition does not travel across a supplier’s catalogue. Changing the facestock, adhesive, ribbon or application substrate can put your application outside the recognised conditions. Ask which specific construction and printing system carry the recognition you are relying on.
Need a construction matched to a documented profile? Send your reflow, autoclave or bake profile to Vizlent and ask for the qualifying data.
Where Wash-Off Label Adhesive Fits in Heat-Resistant Labeling
Wash-Off Label Adhesive is the deliberate opposite of a permanent high-temperature grade, and it belongs in this conversation because a hot caustic wash is itself a heat exposure. A wash-off construction is engineered to hold through filling, pasteurization, storage and distribution, then release cleanly under specified wash conditions. Both of those requirements involve heat, pulling in opposite directions, which is what makes the specification difficult.
Returnable glass bottle systems show the tension clearly. Industry practice described by process chemistry suppliers puts bottle washer solutions at roughly 1.5% to 3.0% sodium hydroxide, heated between 60°C and 80°C. A Wash-Off Label Adhesive has to survive a pasteurization tunnel that may run warm and wet, then let go inside that caustic bath without leaving residue on the glass.
- Hold phase: filling, hot fill or pasteurization, condensation, warehouse heat, transport vibration
- Release phase: hot caustic immersion, mechanical agitation, rinse
- Failure modes a Wash-Off Label Adhesive must be tested against: premature edge release in the hold phase, adhesive residue or film fragments in the release phase
Specifying Wash-Off Label Adhesive Without Losing Heat Performance
Plastics recycling applies the same logic with different acceptance criteria. The Association of Plastic Recyclers distinguishes releasing adhesives, which wash off the PET surface and rinse cleanly from the flake, from non-releasing adhesives, which carry adhesive, film and ink into the recycled stream. APR references protocols including PET-EE-01 and PET-CG-02, which is why a Wash-Off Label Adhesive is specified against a protocol rather than against a marketing claim.
The mistake to avoid is assuming a facestock’s heat rating carries over when you switch to a Wash-Off Label Adhesive. Heat resistance is a construction property, so changing the adhesive changes the construction and the rating has to be re-established. Vizlent’s homepage states at the time of writing that its portfolio covers eight custom adhesive formulations including permanent, removable, freezer and wash-off grades.
- Write acceptance criteria before testing: edge lift limit, minimum barcode grade after the hold phase, residue tolerance after wash
- Test the hold and release phases as one sequence, since a heat-aged label releases differently from a fresh one
- Ask whether published wash off adhesive figures come from a named protocol or from internal screening
- Confirm food-contact status separately, since citing 21 CFR 175.105 or 175.125 does not by itself establish compliance
- For a fuller treatment of release adhesives, supplier options and residue testing, see the dedicated Vizlent guide to removing and releasing label adhesives, and scope a returnable programme against the beverage and beer label range
Running a returnable bottle or recyclable PET programme? Ask Vizlent for Wash-Off Label Adhesive samples with the wash parameters you actually run.
Get the Construction Right Before You Order
Heat resistant labeling failures are expensive because they surface late, usually after parts have been through a process and the identification is gone. Specifying facestock, adhesive and print systems together, then testing that combination against written acceptance criteria, removes most of that risk for the cost of a sample roll. The same discipline applies when a Wash-Off Label Adhesive is in scope, with the added step of testing the hold phase and the release phase as one sequence.
Vizlent has manufactured pressure-sensitive label materials since 2011 and states on its homepage that it supplies customers in more than 50 countries, with roll widths published from 30mm to 1300mm and a 7 to 15 day lead time on custom OEM and ODM orders at the time of writing. Send your process temperature, substrate, cycle count and print method and you will get a recommended construction with its data sheet rather than a catalogue. The sequence below is the fastest route from a process profile to a qualified order.
- Submit your specification: substrate, peak and continuous temperature, cycle count, chemical exposure, print method, wash requirements if any
- Receive a recommended construction: facestock, adhesive grade, liner, matched ribbon or toner route
- Request the technical data sheet: with test conditions attached to every published figure
- Test samples against your written acceptance criteria: on your part, through your real process
- Quote at volume: with roll width, core size, wind direction and lead time confirmed
Start the specification with Vizlent, or browse the heat resistant label range and the wider Vizlent knowledge library first.
Frequently Asked Questions
What temperature can heat-resistant printable labels actually withstand?
It depends on the construction, not the label category. Vizlent currently publishes an engineered polyimide construction as continuous to 300°C (572°F) with short spikes to 350°C, and a polyester construction to 150°C (302°F). Metal foil constructions are cited for higher-temperature applications, but a metal facestock does not by itself give the finished label that rating, so confirm the exact construction and its test conditions against the data sheet.
Are vinyl stickers heat resistant enough for oven or engine use?
No. Vizlent currently publishes flexible PVC vinyl at -20°F to 180°F, roughly 82°C at the top end, which excludes ovens, soldering, paint bake and exhaust proximity. Polyester handles the middle range and polyimide the top, so switch families rather than hoping a vinyl construction holds.
How do I print thermal labels that stay legible after heat exposure?
Use thermal transfer with a full resin ribbon rather than direct thermal, because direct thermal media images through a heat-sensitive layer that keeps reacting when heated again. Match the resin chemistry to the facestock, raise printhead energy and slow print speed for dense barcodes. Verify legibility after the actual heat cycle using an applicable method such as ISO/IEC 15416:2025.
What is a Wash-Off Label Adhesive and when do I need one?
A Wash-Off Label Adhesive is a pressure-sensitive grade engineered to hold through the product’s service life and then release cleanly under specified wash conditions. It is used on returnable glass bottles washed in caustic solutions and on PET containers destined for recycling, where adhesive residue contaminates the recovered material. You need one when the reuse or recycling process requires the label or adhesive to release under specified wash conditions.
Can the same label be heat-resistant and wash-off at the same time?
To a degree, and a Wash-Off Label Adhesive in a warm process is one of the harder specifications in label materials. The construction has to stay bonded through hot fill or pasteurization, then released in a caustic bath typically running 60°C to 80°C at around 1.5% to 3.0% sodium hydroxide. Test both phases as one sequence, because heat-aged labels release differently from fresh ones.
Do heat resistant printer labels need a special printer?
Not usually a special printer, but usually a capable one. High-temperature resin ribbons carry ink with a published melting point above 110°C, which calls for industrial printers configured for high printhead energy and reduced speed. Print compatibility depends on the complete print system rather than on the printer model alone.
How should I test heat-resistant printable stickers before ordering volume?
Write acceptance criteria first: an edge lift limit, a minimum barcode grade after exposure, no delamination and no print transfer. Peel adhesion can then be screened using an applicable method such as ASTM D3330/D3330M-04(2025), a peel adhesion test method for pressure-sensitive tape, where the method and specimen configuration suit the construction. The standard itself notes that peel results usually bear no direct relationship to a functional requirement, so treat short trials as screening rather than proof of service life.
Does UL 969 recognition mean any label from that supplier is approved?
No. Recognition applies to the specific evaluated combination of material, ink and printing or imaging process, together with its conditions of acceptability. Those conditions name the application surfaces, use conditions, exposure temperature limits and any chemical exposures, so changing the facestock, adhesive, ribbon or substrate can put the application outside them.